Contact Information
- Gat No.359, Near BSNL Tower, Ambethan Road, Chakan, Pune, Maharashtra - 410501
- +91 9657852282
- info@adirajcoating.com
- GSTIN: 27ABCCA9930F1ZN
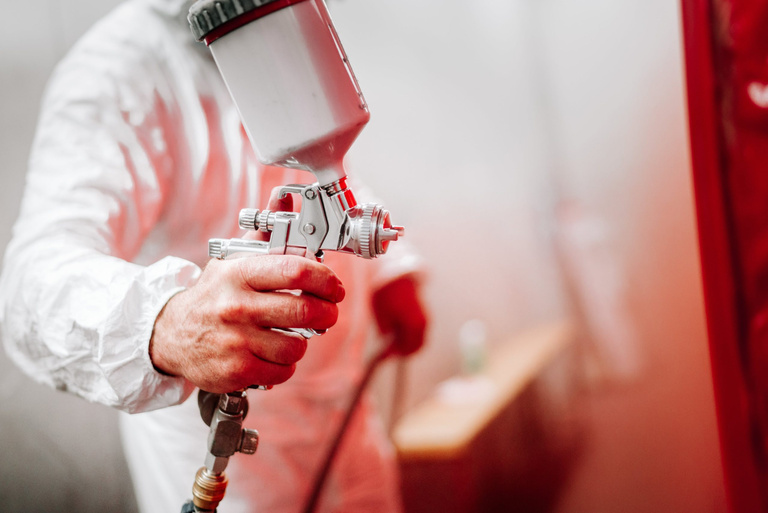
Precision Industrial Automotive Liquid Painting
At ADIRAJ COATING PVT. LTD. (Adiraj Enterprises), our expertise in industrial automotive painting is backed by years of hands-on OEM manufacturing experience and unyielding commitment to finish perfection. Located in Chakan, Pune's automotive heartland, we specialize in high-durability liquid spray finishing systems engineered for Tier-1 automotive and industrial commercial components.
Automotive components endure punishing environmental stresses: intense ultraviolet solar radiation, gravel stone chipping, abrasive road grime, motor oils, thermal cycles, and corrosive humid atmospheres. Our multi-coat finishing systems—incorporating adhesion-promoting chemical pre-treatment, anti-corrosion primer coats, precision-matched base coats, and protective high-solid clear coats—guarantee superior gloss retention, exceptional mechanical elasticity, and long-term surface stability.
Core Technical Strengths
OEM Color Matching
Spectrophotometer-calibrated formulation matching RAL, Pantone, and custom OEM automotive exterior/interior paint shades.
Dust-Free Spray Booths
Pressurized downdraft spray chambers with high-efficiency multi-stage air filtration preventing particulate contamination.
Multi-Substrate Versatility
Engineered surface activation processes for engineering plastics (ABS, PC, PP, Nylon) and ferrous/non-ferrous metals.
Controlled Thermal Curing
Digitally profiled hot air convection bake ovens ensuring total cross-linking, hardness development, and chemical resistance.
Technical Specifications & Standards
Process Technical Parameters
Tier-1 OEM Compliant| Applicable Substrates | ABS, Polycarbonate (PC), PC/ABS alloys, Nylon (PA6/66), Mild Steel (MS), Aluminum, Die-cast components |
| Coating Systems | 2-Component Polyurethane (2K PU), Thermosetting Acrylics, High-Solid Epoxies, Synthetic Enamels |
| Typical Dry Film Thickness (DFT) | Primer: 20 – 35 µm | Base Coat: 15 – 25 µm | Clear Coat: 30 – 45 µm (Total System: 65 – 105 µm) |
| Cross-Hatch Adhesion Test | Class 0 / 5B (ASTM D3359 / ISO 2409) — 100% tape adhesion with zero flaking along lattice cuts |
| Pencil Hardness | ≥ 2H to 3H (ASTM D3363) scratch hardness standard |
| Corrosion Resistance | 480 – 720+ Hours Neutral Salt Spray Resistance (ASTM B117) depending on pre-treatment & primer |
| Gloss Levels Available | High Gloss (>85 GU at 60°), Semi-Gloss (50–70 GU), Satin (25–40 GU), Dead Matt (<10 GU) |
| Curing Cycle | Forced air baking at 70°C – 80°C for plastics; 120°C – 140°C for sheet metal components |
| Testing Equipment | Digital DFT Gauge (Elcometer), Glossmeter, Cross-cut tester, MEK Double Rub tester, Impact tester |
Standard Operating Procedure
Pre-Treatment & Degreasing
Components undergo ultrasonic/solvent degreasing and ionization to remove oils, dust, and static charges.
Primer Coat Application
Conductive or non-conductive adhesion promoter/primer is applied to bridge substrate and topcoat layers.
Base Coat & Clear Coat
Automated/manual electrostatic spray guns apply uniform pigment base followed by UV-resistant clear coat.
Baking & Quality Audit
Precision thermal curing in convection ovens followed by DFT, gloss, and adhesion validation before packing.
Typical Automotive Applications
- Exterior Mirror Housings & Skull Caps
- Automotive Bumpers, Grilles & Fascias
- Dashboard Bezels, Trim Mouldings & Consoles
- Commercial Vehicle Grab Handles & Panels
- Fuel Flap Lids & Outer Door Handles
- Engine Bay Plastic & Aluminum Brackets
- 2-Wheeler Mudguards, Side Covers & Visors
- Precision Instrumentation & Control Housings
Finished Automotive Samples
High-definition photographs of components processed in our Chakan industrial plant: