Contact Information
- Gat No.359, Near BSNL Tower, Ambethan Road, Chakan, Pune, Maharashtra - 410501
- +91 9657852282
- info@adirajcoating.com
- GSTIN: 27ABCCA9930F1ZN
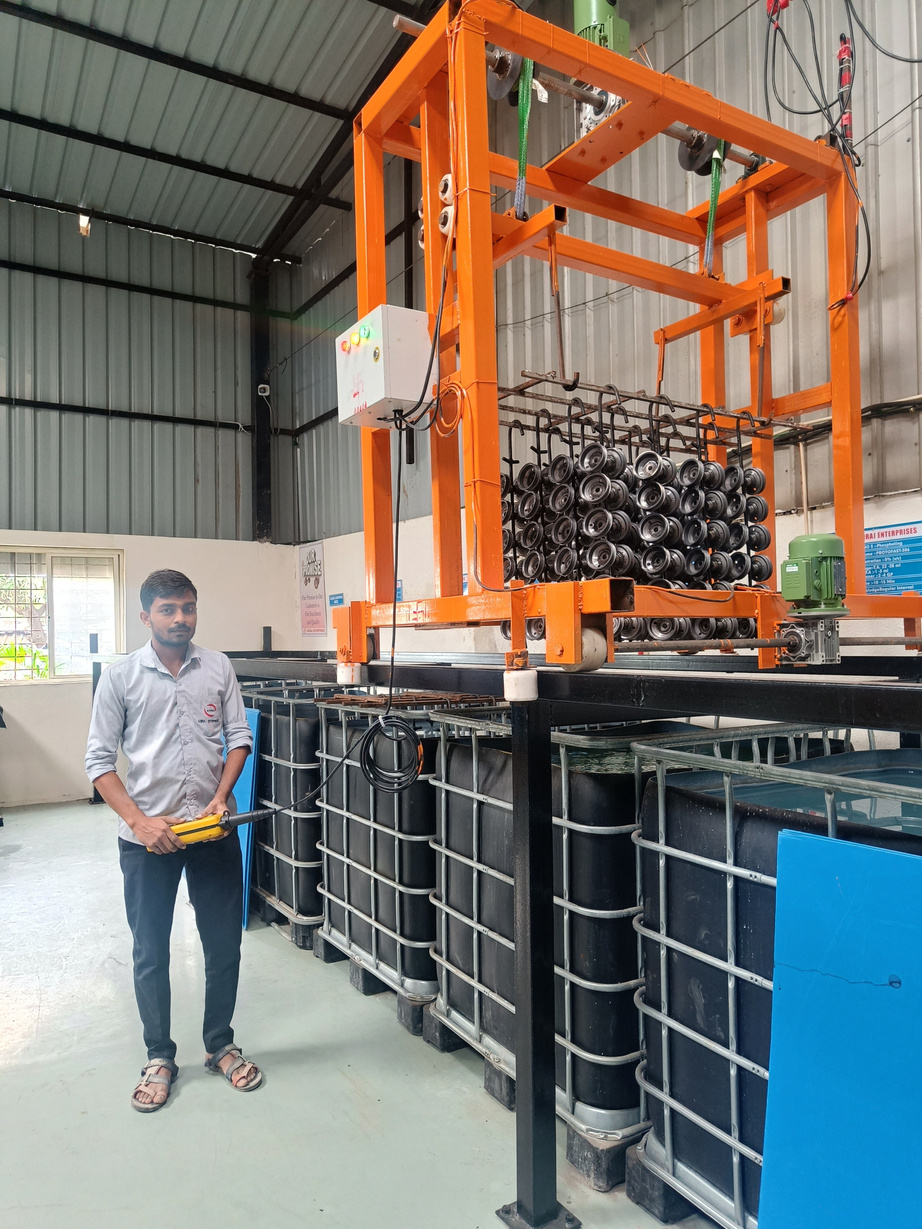
Cathodic Electrodeposition (CED / E-Coat)
ADIRAJ COATING PVT. LTD. in Chakan, Pune provides cutting-edge Cathodic Electrodeposition (CED Coating) services engineered to meet the stringent corrosion resistance mandates of global automotive OEMs. CED coating represents the pinnacle of anti-corrosion science for metal stampings, forged chassis links, and tubular structural assemblies.
The core advantage of CED coating is its electro-chemical deposition mechanism. Metal components are fully submerged in an electrified bath containing water-dispersed epoxy resin particles. As direct electrical current passes between the electrodes and the submerged part (cathode), a dense, uniform polymer film deposits simultaneously over all exterior surfaces, inside hidden tubular cavities, and across sharp laser-cut edges. As the film builds to the target micron thickness (15–25 µm), electrical resistance naturally increases, pushing the coating to deposit into remaining uncoated recessed zones. The result is total encapsulation with zero drip marks, zero runs, and zero unprotected blind spots.
Core Technical Strengths
Extreme Throwing Power
Electrical attraction drives coating deep into internal tubular chambers, hollow box sections, and sharp weld crevices.
1,000+ Hrs Salt Spray
Tested in certified salt spray fog chambers per ASTM B117, routinely exceeding 1,000 hours with negligible creepage.
Micro-Uniform DFT (±2µm)
Unlike spray painting, CED delivers razor-consistent film thickness across complex geometry without puddle buildup.
Eco-Friendly & Closed Loop
Lead-free, waterborne cathodic epoxy bath with multi-stage Ultrafiltration (UF) recovery yields over 98% material efficiency.
Technical Specifications & Standards
CED Process Parameters
ASTM / DIN / JIS Compliant| Applicable Substrates | Cold Rolled Close Annealed (CRCA), Hot Rolled (HR) Steel, Forged Steel, Cast Iron, Galvanized Steel (GI) |
| Bath Chemistry | Waterborne Cathodic Epoxy Resin, Lead-Free, Low VOC, Heavy Metal Free formulation |
| Typical Dry Film Thickness (DFT) | 15 – 25 µm (Microns) standard, tightly controlled to ±2 µm across entire surface geometry |
| Salt Spray Resistance | 1,000+ Hours (ASTM B117) with zero blister formation and less than 1mm scribe creepage |
| Cross-Hatch Adhesion | Class 0 / 5B (ASTM D3359 / ISO 2409) — 100/100 tape adhesion pass |
| Pencil Hardness | 3H (ASTM D3363) scratch resistance |
| Baking / Curing Profile | 160°C – 180°C metal temperature for 20 minutes in continuous convection baking oven |
| Ultrafiltration (UF) System | Multi-stage UF closed-loop dragout recovery ensuring zero paint wastage and superior rinse clarity |
| Role as Primer Coat | Exceptional base primer for subsequent topcoat liquid painting or electrostatic powder coating |
Standard Operating Procedure
Pre-Treatment & Phosphating
Immersion degreasing, pickling, surface activation, and micro-crystalline zinc phosphating with RO rinses.
Cathodic Electrodeposition
Components submerge into electrified bath where cathodic voltage drives uniform epoxy polymer deposit.
UF Rinse & Dragout Recovery
Ultrafiltration permeate rinses wash off uncoagulated resin cream, returning it back into the main dip tank.
Thermal Cross-Linking & Audit
20-minute bake at 170°C cross-links epoxy polymer into an impenetrable shield, followed by DFT verification.
Key Automotive & Engineering Applications
- Automotive Suspension Control Arms & Knuckles
- Chassis Subframes & Front Axle Assemblies
- Brake Calipers, Backplates & Wheel Drums
- Engine Mount Brackets & Transmission Supports
- Seat Sliding Tracks, Recliners & Frame Skeletons
- Deep Stamped Sheet Metal Reinforcements & Braces
- Commercial Vehicle Chassis Outriggers & Hinges
- Heavy-Duty Industrial Fasteners, Springs & U-Bolts
Finished CED Coated Samples
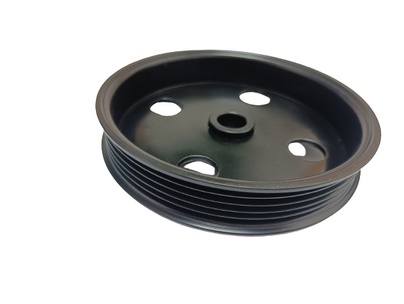
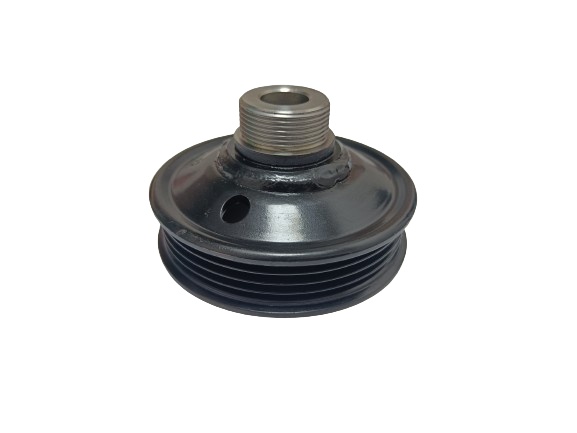
High-definition photographs of components processed in our Chakan industrial plant: