Contact Information
- Gat No.359, Near BSNL Tower, Ambethan Road, Chakan, Pune, Maharashtra - 410501
- +91 9657852282
- info@adirajcoating.com
- GSTIN: 27ABCCA9930F1ZN
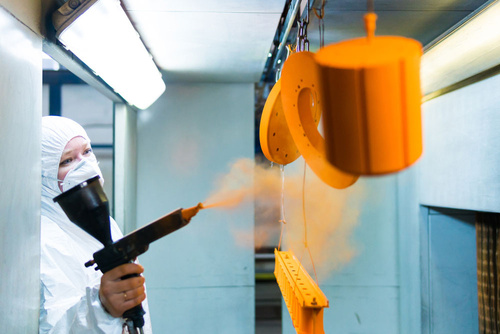
Advanced Industrial Electrostatic Powder Coating
At ADIRAJ COATING PVT. LTD. (Adiraj Enterprises), our state-of-the-art powder coating process ensures 100% even coverage, flawless wrap-around, and long-lasting durability. Located in Chakan, Pune, we serve automotive Tier-1 suppliers, heavy equipment manufacturers, electrical switchgear firms, and precision engineering fabricators across Maharashtra.
Unlike conventional solvent-borne paints, thermoset powder coating involves zero volatile organic compounds (0% VOC), delivering an environmentally compliant, dense polymer shield that is virtually immune to chipping, scratching, hydraulic fluid corrosion, and outdoor ultraviolet degradation. With our disciplined 7-9 tank pre-treatment line and calibrated convection bake ovens, we guarantee maximum molecular adhesion and corrosion barrier properties meeting exacting automotive OEM standards.
Process Advantages & Strengths
7-9 Tank Pre-Treatment
Comprehensive alkaline degreasing, derusting, water rinsing, surface activation, and zinc phosphating for optimum bond strength.
High-Transfer Corona Guns
Calibrated electrostatic charging ensures superior wrap around complex geometric welds, deep louvers, and sharp edges.
Uniform Curing Profile
Digitally monitored convection ovens maintain 180°C to 200°C metal temperature for complete polymer cross-linking.
Versatile Textures & Colors
Pure Polyester, Epoxy-Polyester Hybrid, and Pure Epoxy formulations in smooth gloss, satin, matt, texture, and wrinkle finishes.
Technical Specifications & Standards
Powder Coating Parameters
ASTM / ISO Compliant| Applicable Substrates | Cold Rolled Close Annealed (CRCA) steel, Hot Rolled (HR) plates, Galvanized Iron (GI), Aluminum extrusions, Cast iron |
| Powder Resin Chemistries | Pure Polyester (Architectural/Outdoor), Epoxy-Polyester Hybrid (General Industrial), Pure Epoxy (High Chemical Resistance) |
| Standard Dry Film Thickness (DFT) | 50 – 90 µm (Microns) standard; High-build applications up to 120 µm as per client requirement |
| Salt Spray Resistance | 500 to 1,000+ Hours (ASTM B117) with Zinc Phosphate pre-treatment conversion coating |
| Pencil Hardness | 2H to 3H (ASTM D3363) scratch hardness standard |
| Cross-Hatch Adhesion | Class 0 / 5B (ASTM D3359 / ISO 2409) — 100% tape adhesion pass without peeling |
| Direct & Reverse Impact | ≥ 50 kg·cm (ASTM D2794) with zero flaking or radial cracking |
| Flexibility (Conical Mandrel) | Passes 5 mm diameter mandrel bend without film elongation rupture |
| Curing Cycle | 10 to 15 minutes at 180°C – 200°C metal temperature in calibrated conveyor/batch ovens |
Standard Operating Procedure
Chemical Pre-Treatment
Parts pass through immersion degreasing, descaling, zinc phosphating, and RO water rinses to form a microscopic anchor.
Drying & Masking
Complete moisture evaporation in a dedicated dry-off oven followed by precision high-temp silicone masking of threaded holes.
Electrostatic Spraying
Fluidized powder is sprayed through high-voltage Corona guns, electrostatically adhering in a uniform micron layer.
Thermal Curing & Inspection
Components bake at 180°-200°C for complete flow and cross-linking, verified through DFT and cross-hatch audits.
Key Automotive & Industrial Applications
- Automotive Chassis Brackets & Subframes
- Battery Pack Trays & Enclosures for Electric Vehicles (EV)
- Suspension Links, Stabilizer Bars & Control Arms
- Heavy Commercial Vehicle Structural Hardware
- Electrical Control Cabinets & Switchgear Boxes
- Precision Sheet Metal Fabrications & Stamped Parts
- Automotive Alloy Wheels & Cast Iron Flanges
- Material Handling Racks, Silencers & Pipe Fittings
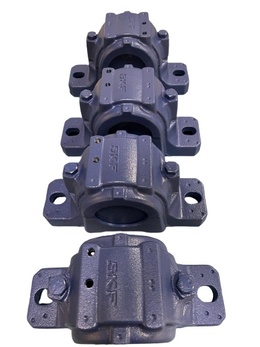
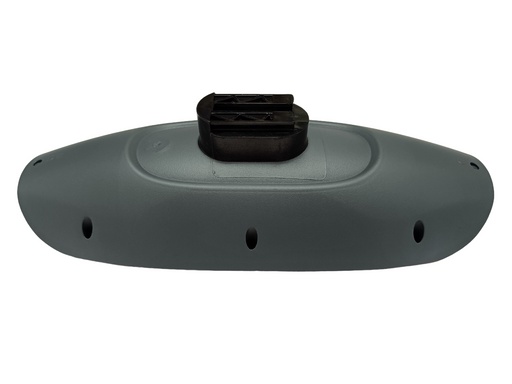
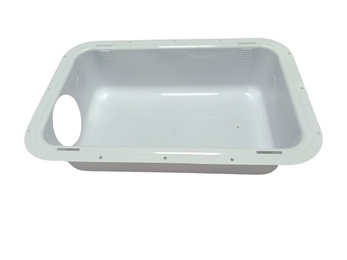
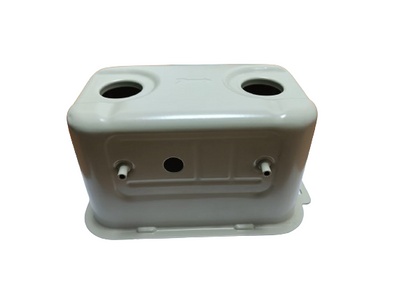
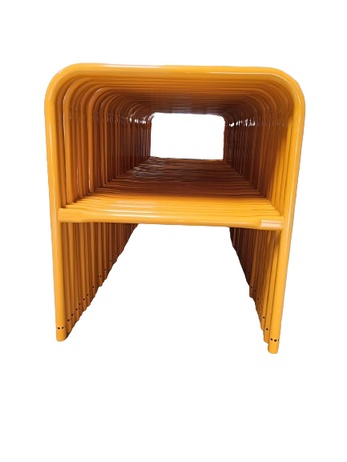
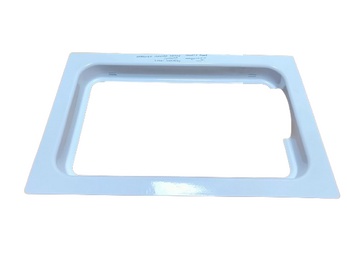
Finished Powder Coating Samples
High-definition photographs of components processed in our Chakan industrial plant: